 No.14 Waihuan Road, CBD, Zhengzhou, China
 +86-18703635966
No.14 Waihuan Road, CBD, Zhengzhou, China
+86-18703635966
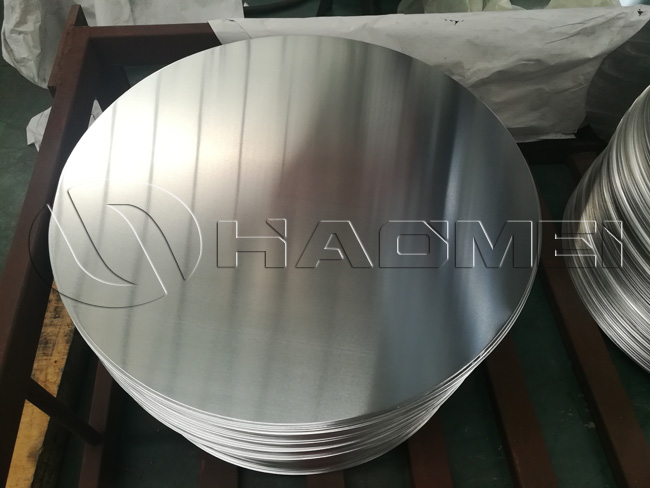
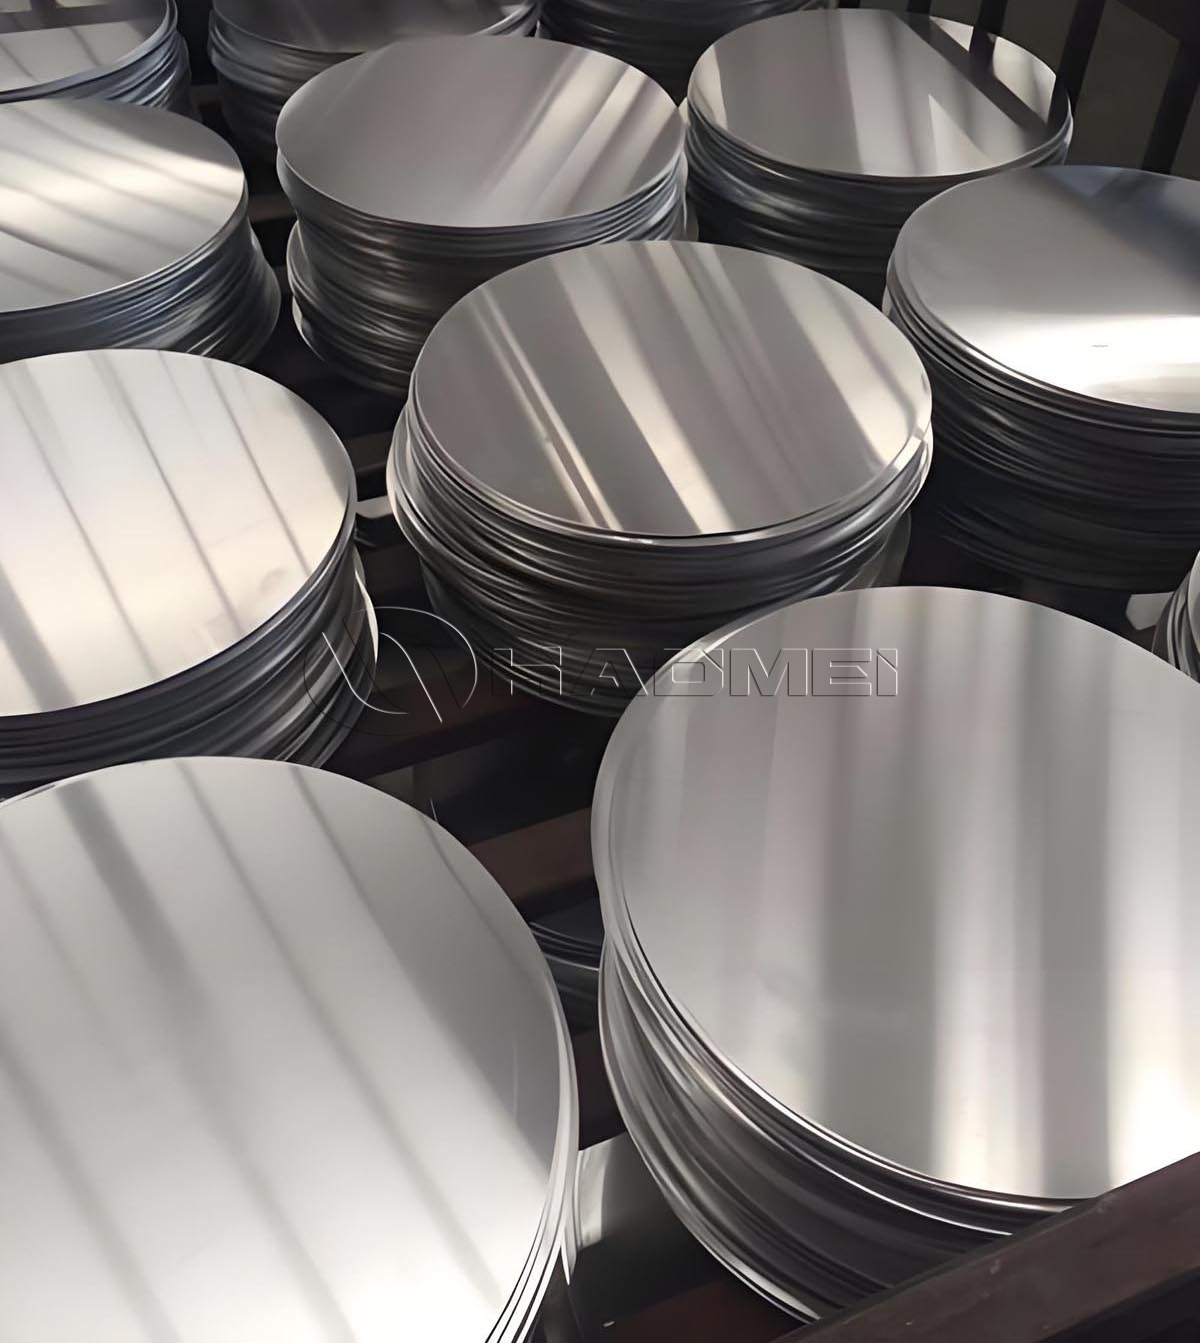
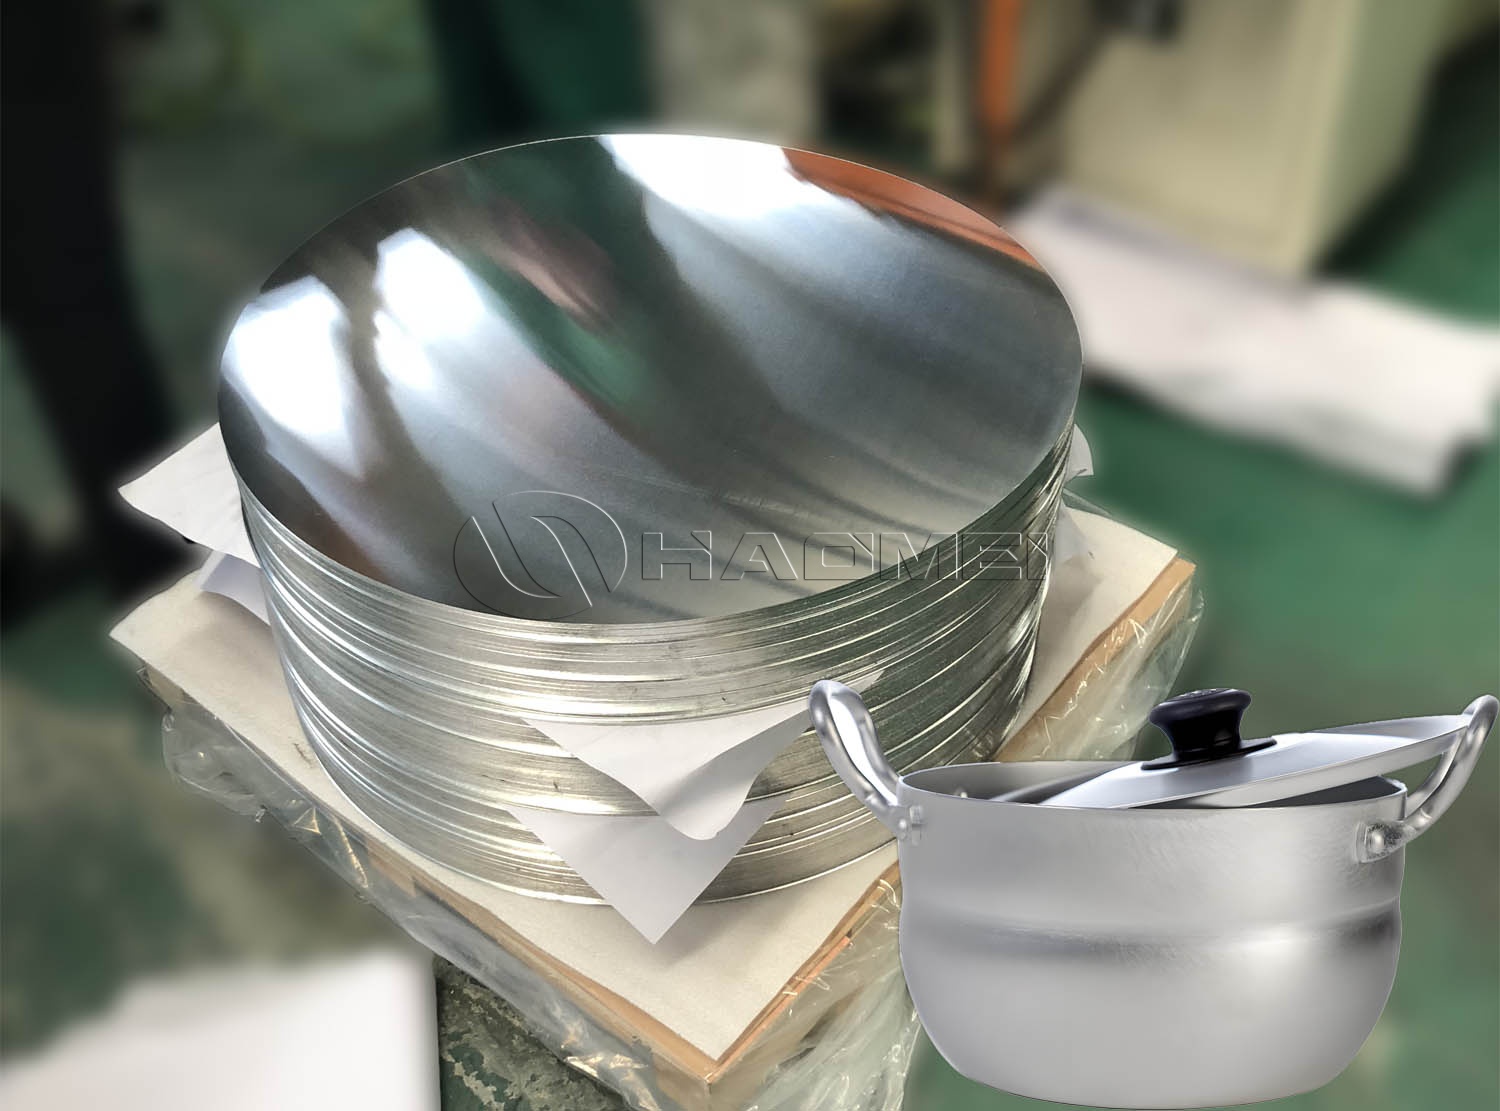
As a manufacturer of aluminum circles and discs, we produce 1050 O-temper aluminum discs specifically for demanding metal spinning operations. These blanks are widely used to manufacture cookware bodies, lampshades, reflectors, ventilation parts, decorative covers, electrical housings, and other rotationally formed components.
For spinning customers, material consistency is more important than nominal thickness alone. A suitable aluminum disc must maintain stable elongation, uniform hardness, controlled grain structure, clean edges, and dependable surface quality from one production batch to the next. Our 1050 O-temper aluminum discs are processed to support smooth deformation during spinning while reducing the risk of cracking, wrinkling, tearing, or excessive surface marking.
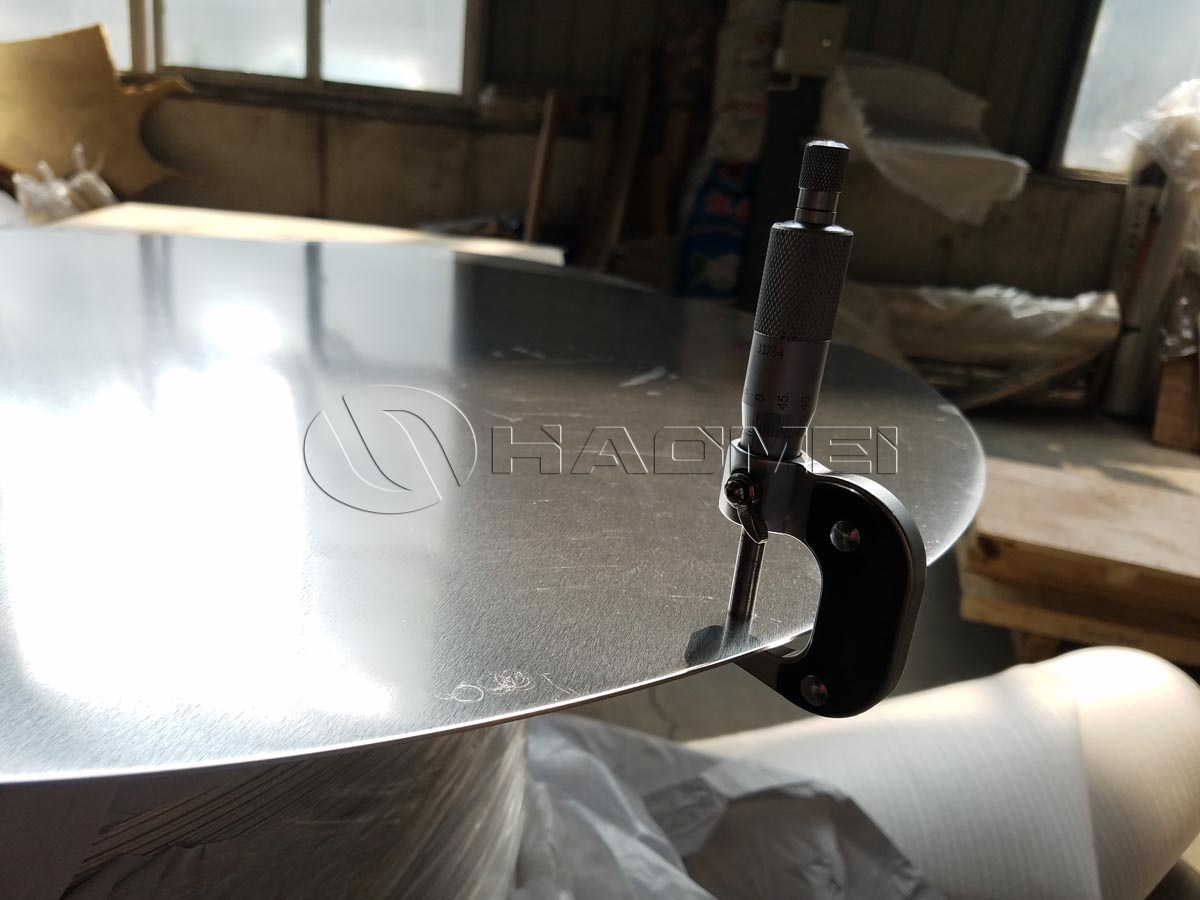
1050 aluminum is a commercially pure aluminum alloy in the 1000 series. Its aluminum content is typically 99.5 percent minimum, providing excellent formability, corrosion resistance, thermal conductivity, and electrical conductivity. Compared with stronger alloy families, 1050 aluminum is softer and more ductile, making it particularly suitable for deep drawing, pressing, and metal spinning.
The O temper indicates a fully annealed condition. During annealing, we carefully control the thermal cycle to relieve work hardening introduced during rolling and blanking. This process restores ductility and gives the aluminum circle blank the softness needed for significant shape change during spinning.
For customers producing deep or complex spun parts, 1050 O-temper aluminum discs offer several practical benefits:
High elongation for demanding deformation during spinning.
Lower risk of edge cracking compared with harder tempers.
Stable response during multi-pass spinning operations.
Good surface finish for visible or coated finished parts.
Excellent corrosion resistance for household, lighting, and industrial applications.
Good thermal transfer for cookware and heat-related components.
We manufacture each 1050 Aluminum Circle with process controls matched to the intended forming method, diameter range, thickness, and final part geometry.
The following table shows common manufacturing ranges for our aluminum discs for metal spinning. Final specifications can be adjusted according to customer drawings, forming trials, and purchasing standards.
| Parameter | Typical Specification | Notes |
|---|---|---|
| Alloy | AA 1050 | Aluminum content 99.5 percent minimum |
| Temper | O / H0 | Fully annealed for high formability |
| Thickness | 0.50-6.00 mm | Custom thicknesses available by agreement |
| Diameter | 100-1,200 mm | Larger diameters available subject to equipment capability |
| Diameter tolerance | Typically +/-0.5 mm to +/-2.0 mm | Depends on disc diameter and thickness |
| Thickness tolerance | According to agreed standard | Controlled from incoming coil through final inspection |
| Surface | Mill finish, bright finish, or specified finish | Free from defects that affect spinning performance |
| Edge condition | Smooth, burr-controlled, crack-free | Important for stable spinning and safe handling |
| Flatness | Controlled for blanking and forming | Verified according to disc size and application |
| Tensile strength | Typically 60-95 MPa | Actual values depend on thickness and annealing condition |
| Elongation | Typically 25 percent minimum | Values vary with gauge and test method |
| Packaging | Paper interleaving, moisture protection, pallet | Export packaging available |
Chemical composition is controlled in accordance with applicable standards and customer requirements. While 1050 aluminum is known for its purity and formability, the final spinning result also depends on blank dimensions, lubrication, tool design, spinning speed, reduction ratio, and the geometry of the finished component.
Our production process begins with qualified 1050 aluminum coil. We evaluate incoming material for alloy conformity, surface condition, thickness consistency, and coil shape before it enters our aluminum circle processing line. This material discipline is essential because spinning defects can originate from inconsistent coil properties long before the disc reaches the forming machine.
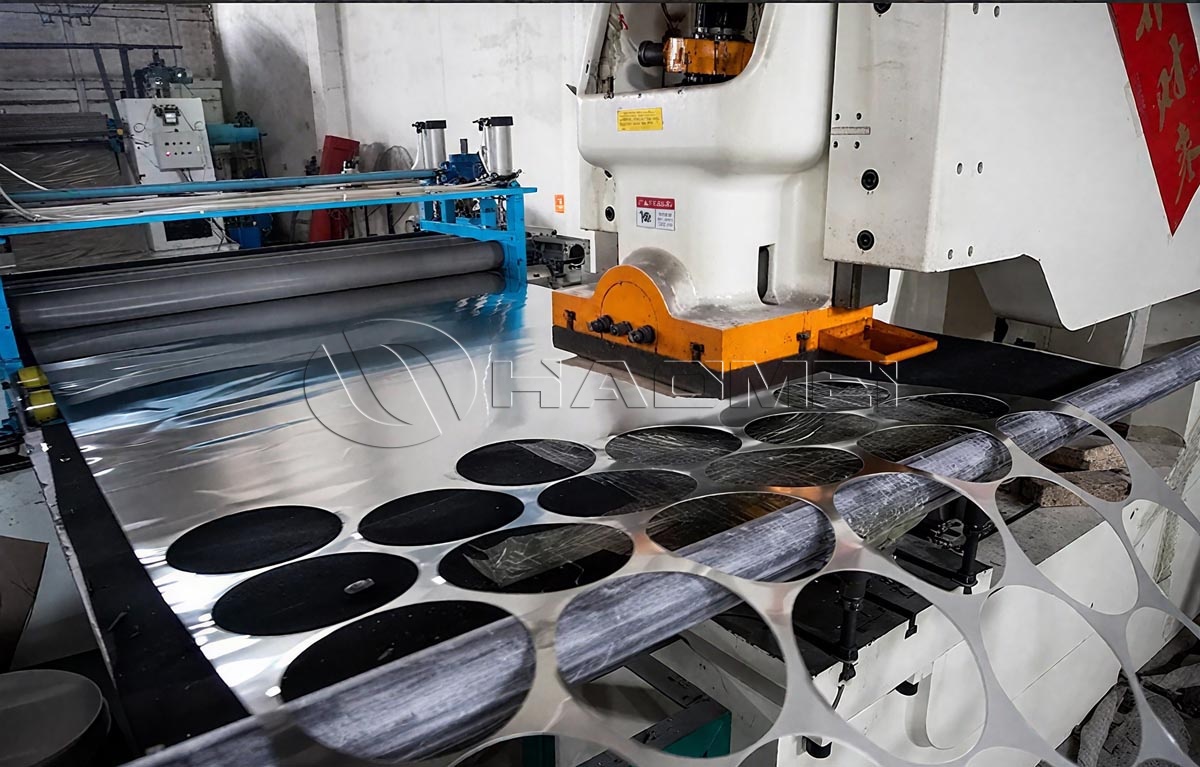
Coils are slit or prepared according to the required blank diameter and production route. We select processing parameters to minimize edge damage and maintain stable material flow into subsequent blanking operations.
We use controlled blanking equipment to produce circular aluminum discs with clean geometry. The cutting process is adjusted to achieve a smooth edge condition with limited burr formation. For spinning operations, edge quality is particularly important because localized edge damage can develop into cracks under rotational forming stress.
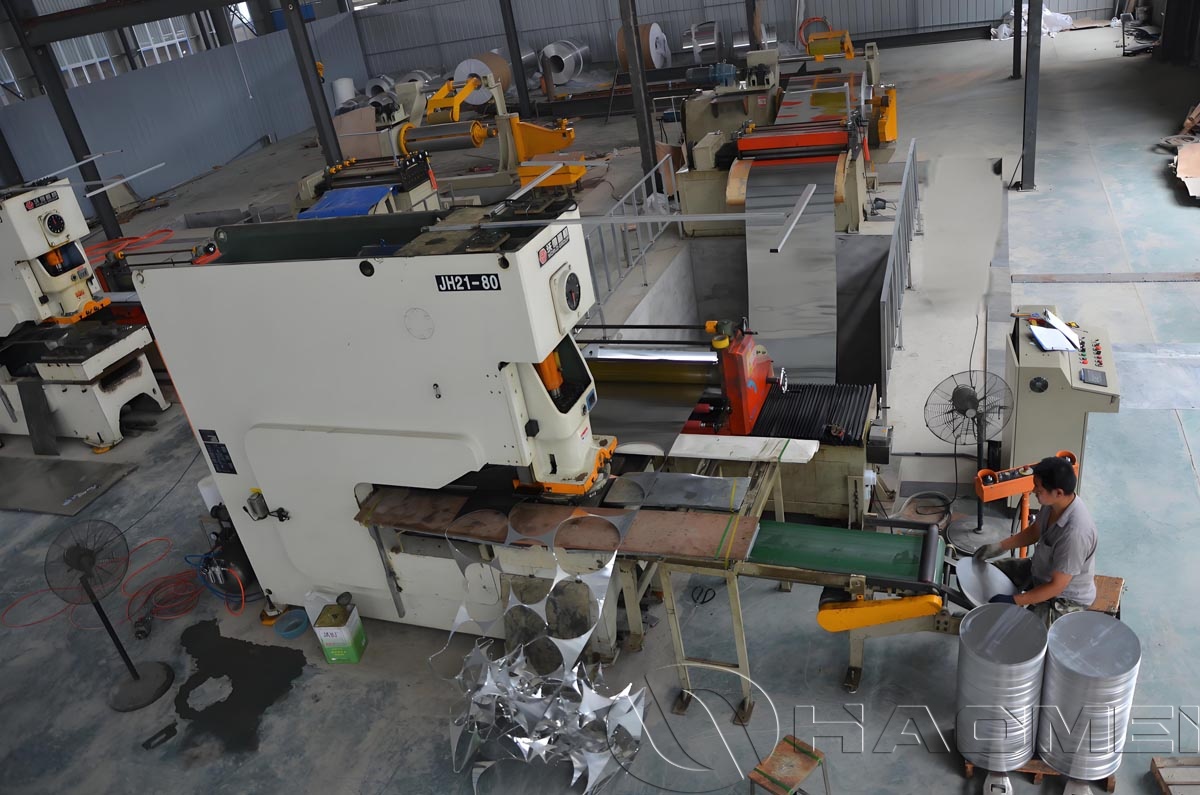
After rolling and blanking-related strain, the discs undergo annealing to achieve the O-temper condition. Our annealing process is managed to support uniform softness and stable elongation across the complete disc surface. Inadequate annealing can result in uneven forming behavior, while excessive or inconsistent heat treatment may affect surface quality and dimensional stability.
We inspect diameter, thickness, surface condition, flatness, edge quality, and packaging condition before shipment. Where required, we can apply additional inspection criteria based on the customer's spinning process, such as limits for scratches, oil residues, edge burr, or local deformation.
A 1050 aluminum circle for spinning must perform consistently under localized pressure and continuous rotation. We therefore focus on the quality features that directly influence the customer's forming efficiency.
Variation in hardness across a batch can cause inconsistent material flow. One disc may spin smoothly while another may wrinkle or crack under identical tooling conditions. We control annealing and raw material selection to provide stable O-temper properties for repeatable production.
A rough or heavily burred edge can initiate cracks during spinning, especially where the part requires substantial draw depth or edge curling. Our blanking controls are designed to produce edges suitable for subsequent forming operations.
For lampshades, decorative housings, cookware, and reflective products, surface quality affects both manufacturing efficiency and final appearance. We supply aluminum disc blanks with protected surfaces and appropriate interleaving options to reduce transit damage and handling marks.
Good flatness supports secure clamping and accurate centering on spinning equipment. Controlled disc geometry helps reduce vibration, improves wall thickness distribution, and supports a stable forming cycle.
Our 1050 O-temper aluminum discs are supplied to manufacturers producing a broad range of rotationally formed parts. Common applications include:
Cookware bodies, pans, pots, and lids.
Lampshades, lighting reflectors, and decorative light covers.
Ventilation covers, fan components, and ducts.
Industrial equipment housings and end caps.
Chemical and food processing containers.
Architectural decorative components.
Electrical enclosures and protective covers.
Automotive and transportation trim parts.
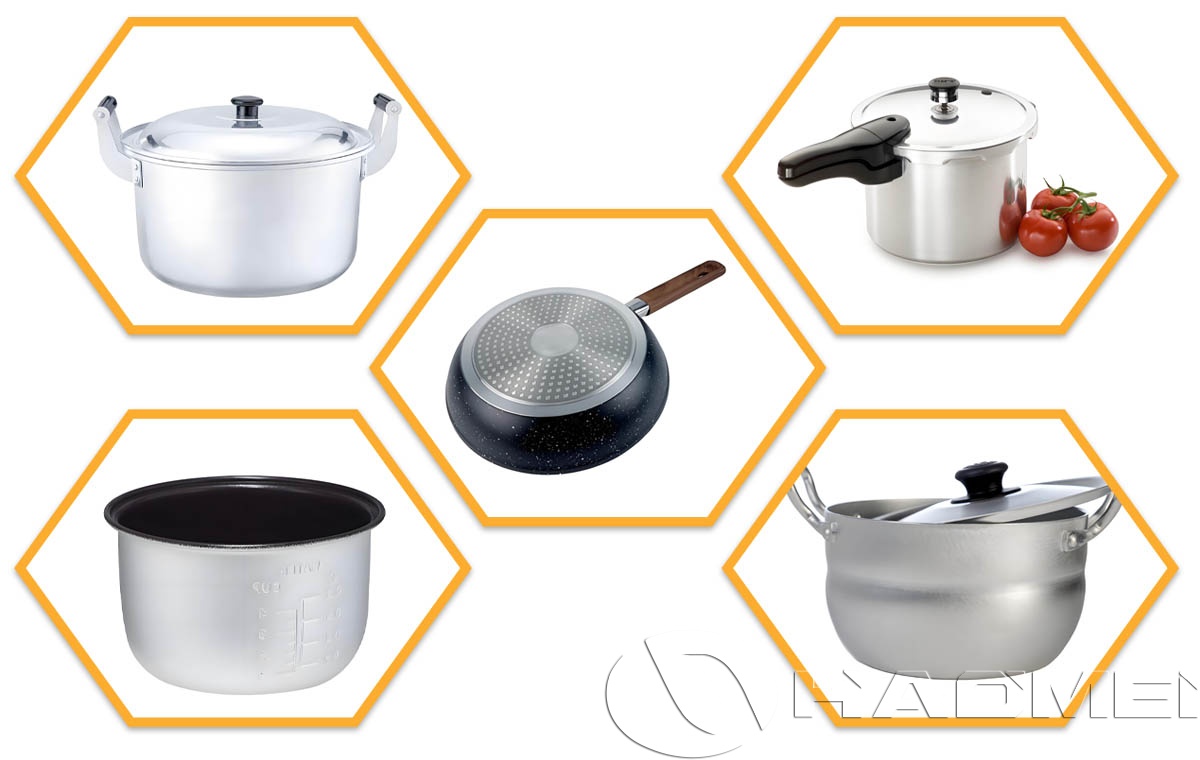
For customers requiring a wider range of purity grades or tempers, our 1000 Series Aluminum circle production program also includes alternatives selected according to formability, surface, and application requirements.
The correct spun aluminum disc begins with an accurate blank calculation. Diameter must allow sufficient material for the finished profile, flange, trimming allowance, and expected wall thinning. Thickness selection should consider the final part stiffness, depth of draw, tool radius, spinning method, and any post-forming operations such as polishing, anodizing, coating, or welding.
When evaluating a new project, we recommend that customers provide the following information:
Finished part drawing or sample.
Required alloy and temper.
Disc diameter and thickness, if already defined.
Spinning method, such as conventional spinning or shear spinning.
Surface finish requirements.
Dimensional tolerances and inspection standards.
Annual or monthly order quantity.
Packaging, labeling, and export destination requirements.
Our technical team can review these details and recommend a practical aluminum circle blank specification for trial production or regular supply.
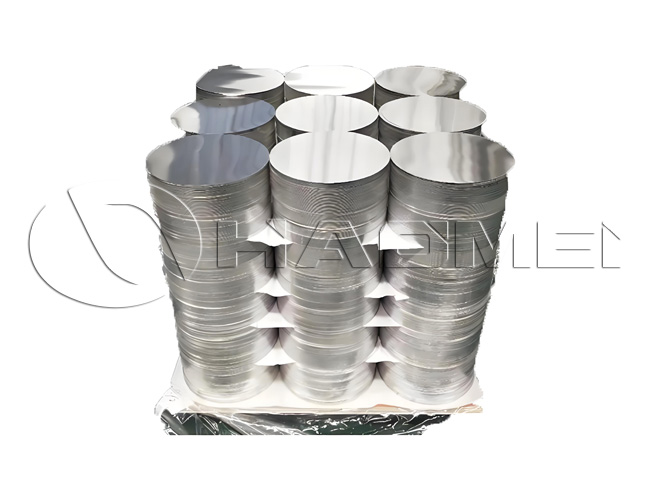
Aluminum discs must be protected from moisture, friction, contamination, and deformation during storage and transportation. We package 1050 O-temper aluminum discs using suitable paper interleaving, protective wrapping, desiccant where required, reinforced outer protection, and wooden pallets for export shipments.
For large-diameter discs, we arrange packaging to reduce movement and prevent edge damage. For thinner materials, stacking height and pallet support are controlled to avoid distortion. Each package can be labeled with alloy, temper, size, batch number, quantity, and customer-specific identification details.
As a factory producing aluminum circles for spinning applications, we manage material selection, blank production, annealing, inspection, and export packaging within a controlled manufacturing system. This direct production approach allows us to align the disc specification with the actual forming requirements of our customers.
Whether you require standard 1050 O-temper aluminum discs or customized aluminum circle blanks for a new spinning project, we can provide technical confirmation based on your dimensions, application, and quality expectations. Our objective is to supply stable, formable material that supports efficient spinning performance and consistent finished products.
Office Address:
No.14 Waihuan Road, CBD, Zhengzhou, China
Contact Us
HAOMEI Aluminum offer an custom aluminum circle for you!
whatsapp: +86-18703635966
Email: sales@alummc.com
Email: alummc@hotmail.com
Request Free Sample & Quotation
Copyright © 2026 By HAOMEI Aluminum CO., LTD. All Rights Reserved. Sitemap
 +86-18703635966
 sales@alummc.com
 8618703635966
